

Building an open-front stackable parts bin
Difficulty: easy. Time: 10 minutes design, 30 minutes making. Best method: laser-cut plywood.
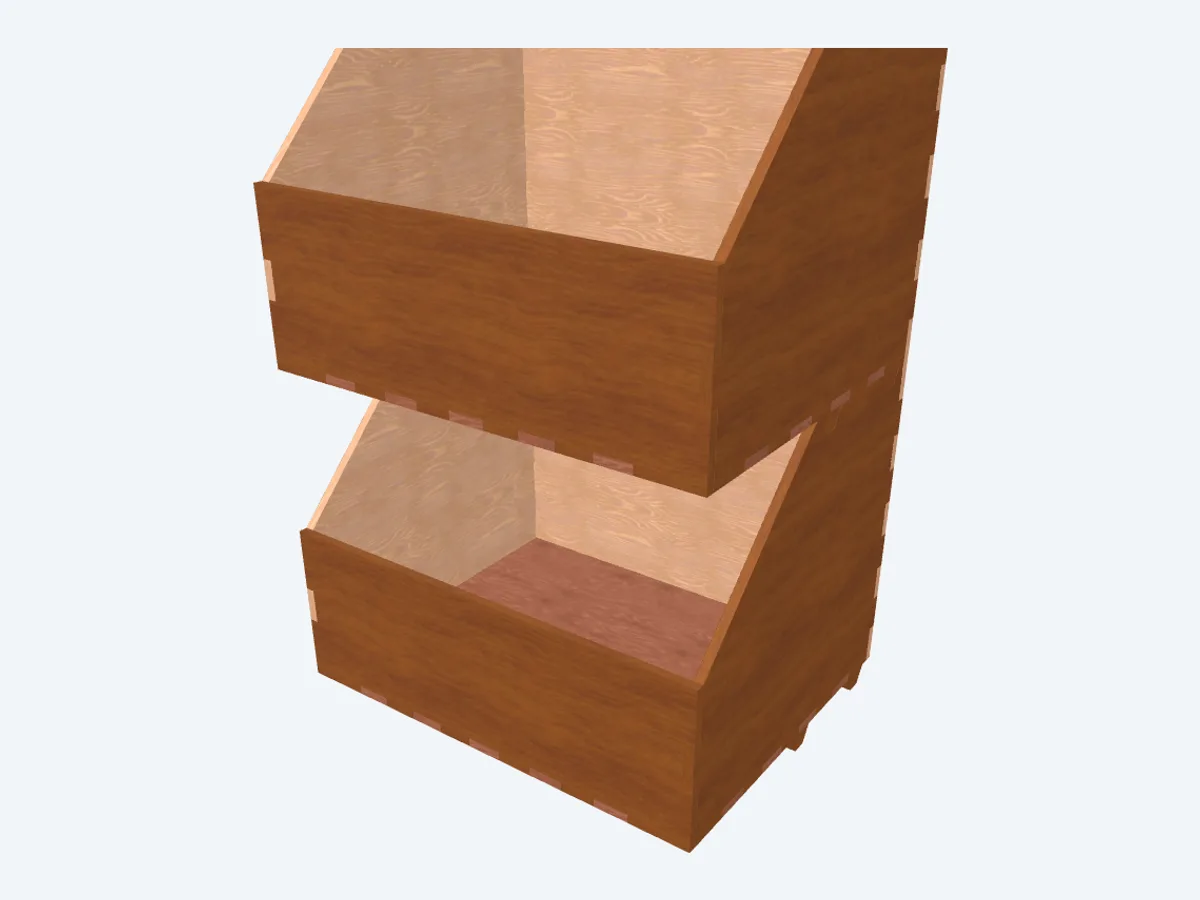
A parts bin is a friendly laser project: a tall back, a low slanted front, two sloped side walls, and a floor that all lock together with finger joints. The slanted front makes it easy to scoop parts in and out, and a row of matching bins keeps a bench tidy. The Assembled 3D tab shows the panels in place so you can judge size before spending a sheet.
What you need
- Laser cutting: 3 to 6 mm plywood or MDF. Measure the actual sheet thickness with calipers, it is rarely exactly 3 mm.
- 3D printing: any rigid filament. 4 to 6 mm panels print stronger joints than laser-thin ones.
- Glue: PVA wood glue for plywood, plus a couple of clamps or elastic bands
1. Bin size
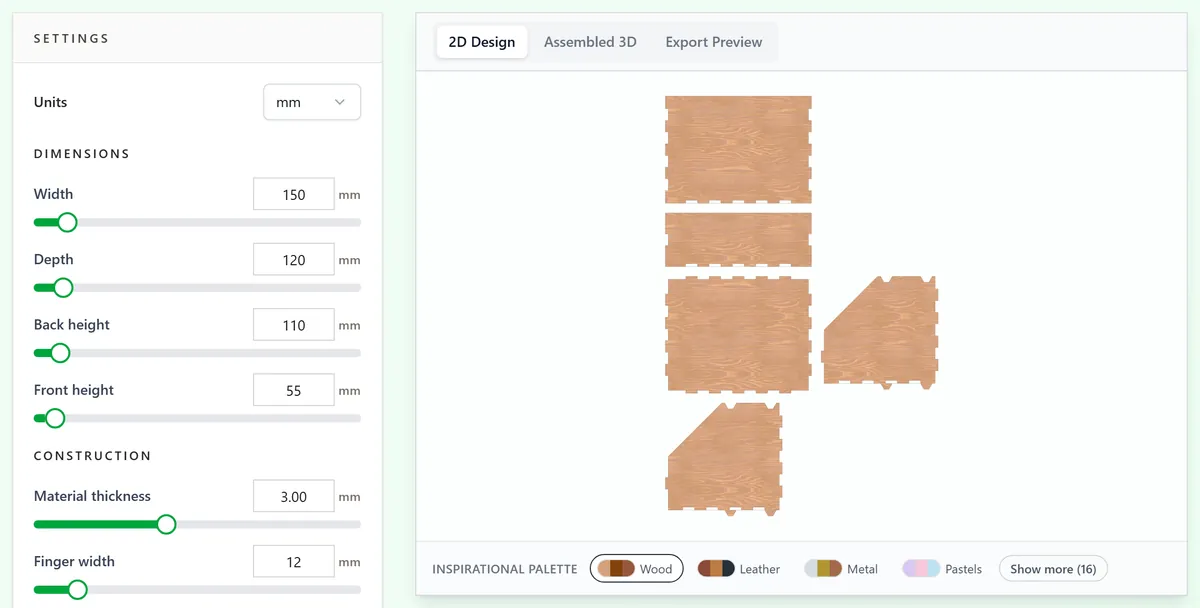
Width and Depth are outside dimensions, so subtract two material thicknesses to get the usable interior. Thickness must match your sheet, because every finger joint is derived from it.
2. Shape the opening
- Back height sets the tall rear wall of the bin.
- Front height sets the short front wall. The side walls slope from the back down to the front to make an open scoop.
- Finger width controls the size of the interlocking joints along every edge.
3. Check the assembly
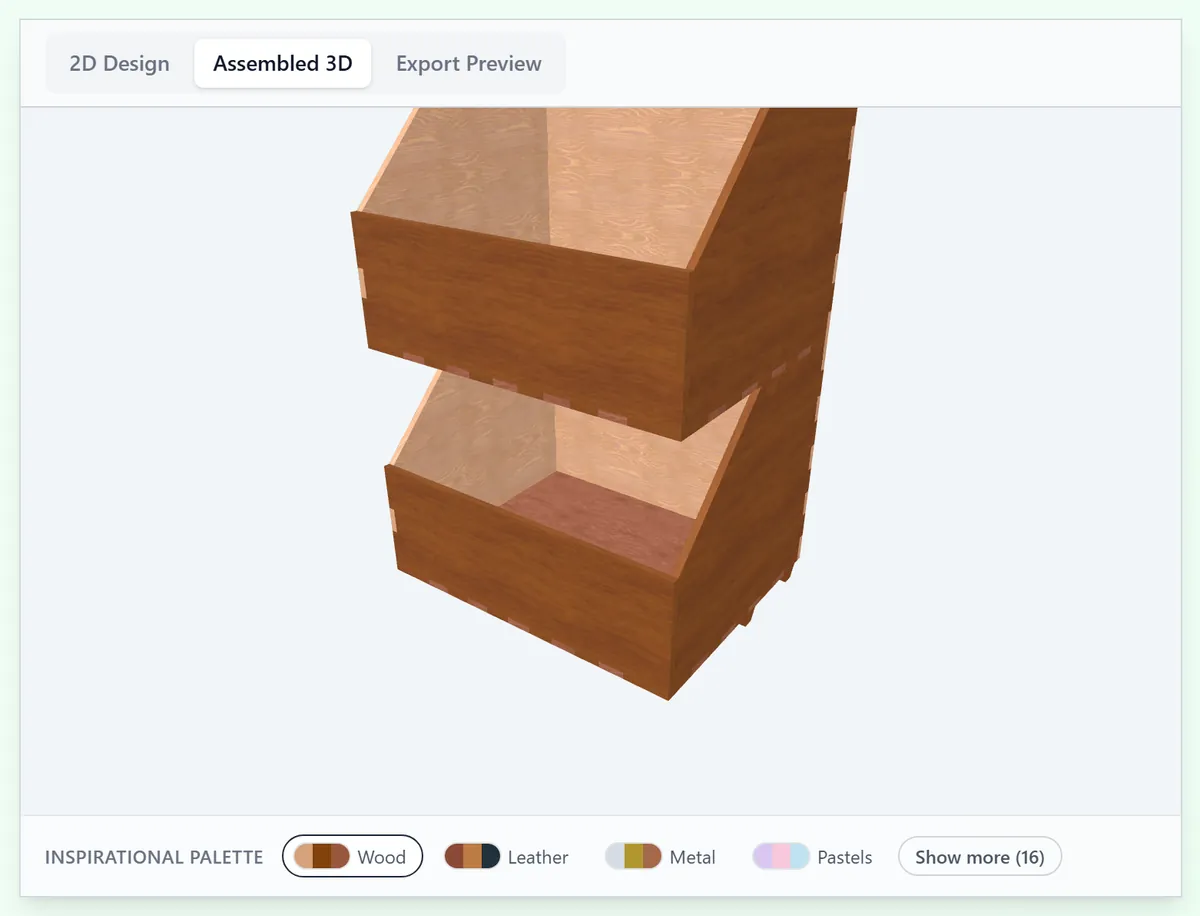
Switch to the Assembled 3D tab and orbit the bin to catch a front that sits too high or a bin that is deeper than you meant. The Export Preview tab shows the flat sheet with each panel in its own colour.
Choose your build method
Laser cutting
Before you cut
- Measure your sheet with calipers and set Thickness to what you measured, not what the label says.
- Run a joint test first on a new sheet: cut one side and the floor, dry fit them, and only commit the rest once the tabs seat with light hand pressure.
- Keep the panels in the layout order so the sloped sides do not get mirrored by accident.
Glue up
- Dry fit everything first. Finger joints in charred ply need a light sanding on the tabs, not force.
- Glue the back, front, and two sides into a ring and check the slant sits square before the glue grabs.
- Drop the floor in last and clamp across the bin until the glue is cured.
3D Printing
Slice and print
- The 3D download is a zip with one part per panel, numbered to match the flat sheet order.
- Every part is already extruded to the Thickness value. Do not scale the parts in the slicer: it changes the joint sizes too.
- Lay each panel flat on the bed so the joints print without supports.
- Print at 0.2 mm layers with 3 or more perimeters so the finger joints come out strong.
Next steps and project ideas
- Engrave a label on the tall back wall before cutting so each bin is easy to find.
- Cut a matching row of bins in different widths for a modular bench organiser.
- Add small feet or a lip so the bins nest neatly when you set one on top of another.
Take the design into your software
Was this guide helpful?
More in Boxes and storage
Keep up with MyLaserTools.
Email me about new tools, product updates, tutorials, and occasional MyLaserTools offers. Unsubscribe at any time.
© 2026 MyLaserTools.com. All rights reserved.